A pharmaceutical production changeover is the controlled transition from one batch, 製品, 強さ, サイズ, or packaging format to the next run. It can include line clearance, クリーニング, 部品を交換する, tooling setup, machine adjustments, recipe changes, startup trials, 検査, and restart verification.
Poorly controlled changeovers increase downtime and the risk of mix-ups, residues, incorrect settings, 梱包ミス, or unstable startup. The objective is not simply faster tooling replacement, but a controlled return to routine production.
What Is a Pharmaceutical Production Changeover?
A pharmaceutical production changeover is the complete process of converting a machine or production line from one defined production condition to another.
The International Society for Pharmaceutical Engineering (ISPE) separates changeover into clean-up, set-up, and start-up, making clear that setup alone is only one part of the transition.
What Does “Changeover” Mean in Pharmaceutical Production?
Changeover covers the controlled work needed to close the previous run, configure the next one, and restore acceptable production.
Typical activities include material removal, ラインクリアランス, クリーニング, replacement of tooling or format parts, adjustment of guides and sensors, selection of the correct Human-Machine Interface (HMI) or Programmable Logic Controller (PLC) レシピ, and restart verification.
Where Does Changeover Start and End?
Changeover needs consistent start and end points if changeover time is to be compared meaningfully.
A site may start timing when the previous run stops and finish after the new setup passes restart checks. A same-product size change, product-to-product changeover, and end-of-campaign change can require different cleaning, クリアランス, 設定, and verification scopes.
Changeover vs Line Clearance vs Cleaning
Changeover is the complete transition; line clearance and cleaning are separate controls within it.
| 活動 | 主な目的 | Typical Scope | Main Risk Controlled |
| 切り替え | Move to the next approved condition | Clearance, クリーニング, 部品を交換する, 設定, startup, 検証 | Incorrect transition and downtime |
| Line clearance | Remove previous or unnecessary items | 製品, コンポーネント, printed materials, 書類, 無駄 | Mix-ups and wrong materials |
| クリーニング | Remove residues and contaminants | 製品接触部, 装置, defined areas | Carryover and contamination |
An empty-looking line is not automatically clean, and cleaned equipment is not automatically cleared of previous labels or documents.
What Are the Main Steps in a Pharmaceutical Production Changeover?
A controlled changeover moves from closing the previous run through clearance, クリーニング, equipment setup, startup verification, and release for routine production.
Stop the Previous Batch and Remove Remaining Materials
Close the previous run before introducing the next configuration. Remaining product, packaging components, 拒否します, samples, 無駄, and work-in-process should be handled according to the approved procedure.
Complete Line Clearance
Line clearance confirms that previous or unnecessary materials and information will not enter the next operation. European Union Good Manufacturing Practice (欧州連合 GMP) 章 5 requires packaging lines and equipment to be free of previous products, 材料, or documents not required for the current operation, using an appropriate checklist.
Clean the Equipment and Production Area
Cleaning removes residues and contamination according to the applicable procedure. FDA’s cleaning-validation inspection guide recognizes that same-product batches and product changes can use different cleaning processes when written procedures clearly define when each applies.
Replace Change Parts, ツーリング, and Product-Contact Components
Install the parts required for the next product or package format. Examples include punches and dies, capsule-size parts, ブリスター型, ボトルガイド, starwheels, capping components, carton guides, and pouch-format parts.
Adjust Machine Settings and Load the Correct Recipe
Physical parts and electronic settings must match the same approved format. HMI or PLC recipes can store parameters, but they do not verify physical tooling. For GMP-relevant electronic recipes, アクセス, configuration changes, and audit trails should follow validated computerized-system controls.
Run a Startup Trial and Verify the New Setup
A startup trial or verification run confirms that the new setup can produce acceptable output. Checks can include filling, 形にする, closure or sealing, コーディング, 検査, and reject functions.
Release for Routine Production
Changeover is complete only after the required setup and restart checks are satisfied. The first product moving through the machine is not necessarily the endpoint.
[IMAGE 2 PLACEHOLDER — Pharmaceutical Changeover Workflow]
What Is Line Clearance in the Pharmaceutical Industry?
Line clearance in the pharmaceutical industry is the controlled check that previous or unnecessary products, 材料, コンポーネント, and information have been removed before the next applicable operation begins.
It matters especially on packaging lines where different products, strengths, ラベル, カートン, チラシ, and printed components may share the same area.
What Must Be Removed During Line Clearance?
Line clearance should remove items from the previous operation that are not required for the current one. Depending on the standard operating procedure (SOP), this can include product, packaging components, ラベル, カートン, チラシ, rejected items, coding samples, 書類, status labels, and waste. EU GMP specifically includes previous products, 材料, and documents not required for the current packaging operation.
What Equipment and Area Checks Are Required?
Line clearance should cover places where previous-run items can remain unnoticed, not only visible machine surfaces. Typical checks include feeders, コンベア, ガイドレール, machine recesses, coding stations, 検査システム, reject chutes, and accumulation areas.
ラベル, Printed Materials, and Documents to Verify
Printed packaging materials require close control because an incorrect label, カートン, リーフレット, or variable code can create a product mix-up. EU GMP requires packaging operations to minimize cross-contamination, 取り違え, and substitutions.
米国では, 21 CFR 211.130 requires pre-use inspection to confirm that previous drug products and unsuitable packaging or labeling materials have been removed, with the inspection documented.
Who Performs and Confirms Line Clearance?
Responsibility should be defined by the manufacturer’s approved procedures and pharmaceutical quality system. The SOP should specify trained or authorized personnel, who performs the inspection, who records it, and whether separate verification is required.
Common Line Clearance Mistakes
Failures usually come from incomplete physical inspection rather than missing paperwork. Typical examples are signing before inspection, checking only visible surfaces, leaving labels near the printer, overlooking reject areas, or restarting before discrepancies are resolved.
[IMAGE 3 PLACEHOLDER — Pharmaceutical Line Clearance Checks]
What Equipment Settings and Change Parts Must Be Adjusted?
Pharmaceutical equipment changeover varies by machine because each process uses different tooling, format parts, product-contact components, センサー, and mechanical adjustment points.
| 装置 | Typical Change Parts | Main Adjustments | Restart Focus |
| 錠剤プレス | パンチ, 死ぬ, force-feeder | Fill depth, feeder height, 予圧縮, メイン圧縮, 錠剤の厚さ | タブレットの重量, 厚さ, 硬度, 排出 |
| カプセル充填機 | Capsule segments, 投与ディスク, タンピングピン, locking components | Dosing depth, 空の, カプセルの分離, locking position | カプセルの分離, fill consistency, ロック, 拒絶 |
| ブリスター包装機 | Forming mold, ガイドトラック, feeder parts, sealing plate/roller, punching die | Forming depth, index pitch, sealing temperature/pressure, feeding position | Cavity forming, 餌やり, 封印, 切断 |
| Tablet Counting And Filling Machine | Bottle guides, Discharge nozzle,シリンダー,counting platform | Vibration frequency, counting platform height, guide rail width | Stable product feeding, bottle positioning and count accuracy |
| 箱詰め機 | Carton magazine, carton conveying guides, carton-opening mechanism, pusher components, ear-folding and carton-closing components | Conveyor width, pusher position, carton-opening position, folding and closing position, inspection position | Stable carton feeding, reliable carton opening, accurate product insertion, correct folding and sealing, and inspection accuracy |
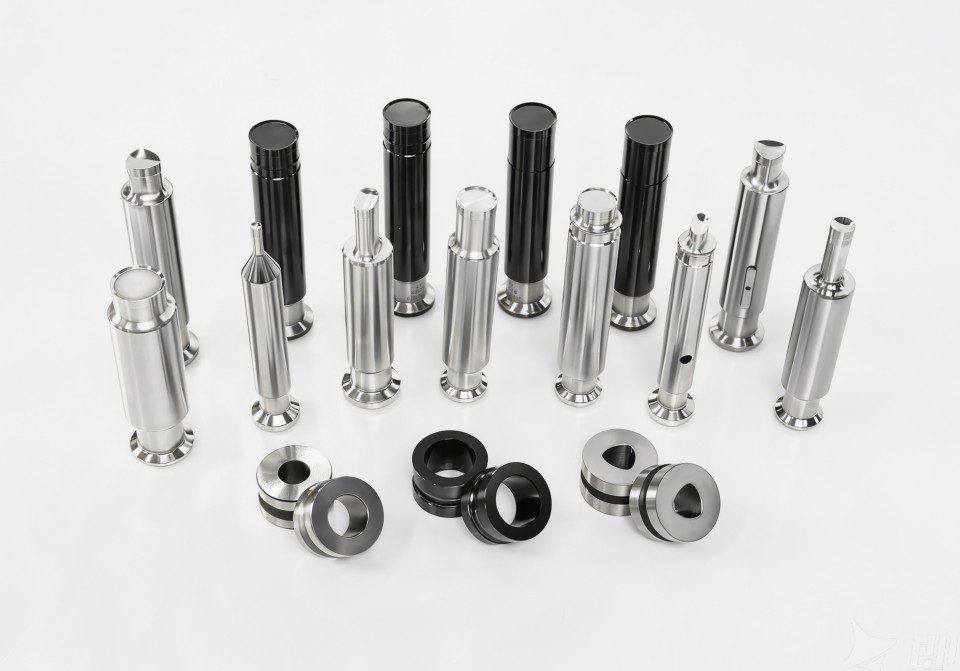
Tablet Press Changeover
Tablet compression equipment changeover mainly involves punches, 死ぬ, feeder components, と圧縮設定. Besides tooling replacement, operators may need to reset fill depth, The gap between the feeder and the turntable, 予圧縮, main compression and ejection settings.
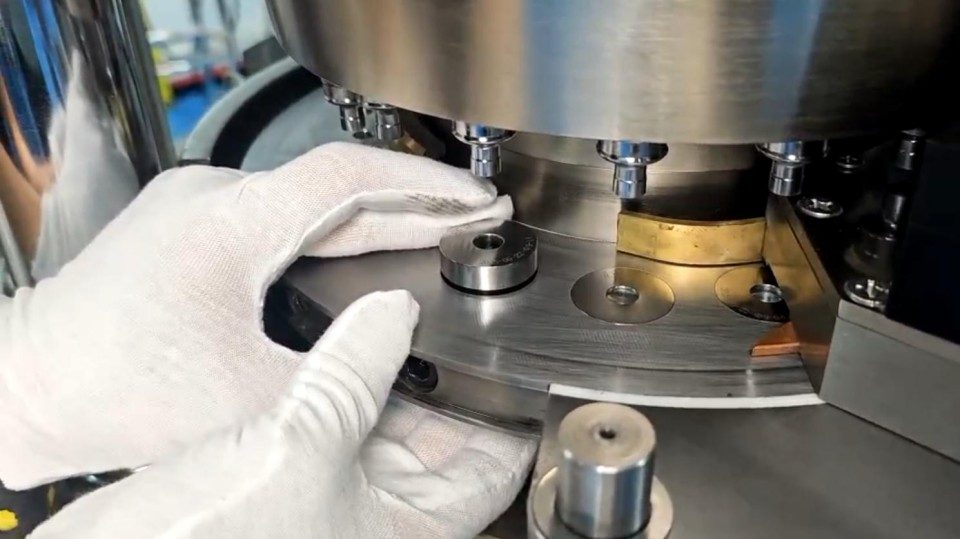
Capsule Filling Machine Changeover
Pharmaceutical capsule filling machine changeover can involve capsule-size segments, 投与ディスク, タンピングピン, vacuum components, and locking parts. Setup normally includes capsule separation, dosing position, 空の, and reject adjustment.
Blister Packaging Machine Changeover
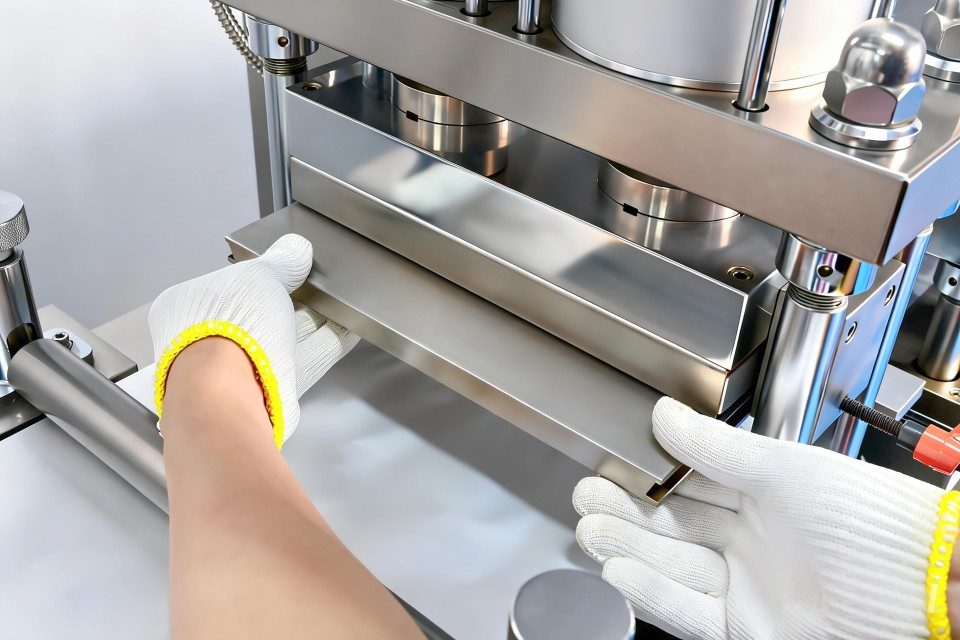
Pharmaceutical blister packaging machine changeover typically affects forming, 餌やり, 封印, indexing, and punching stations. Depending on the blsiter pack format, forming molds, feeder tracks, sealing tools, punching dies, ガイド, and coding may require replacement or adjustment.
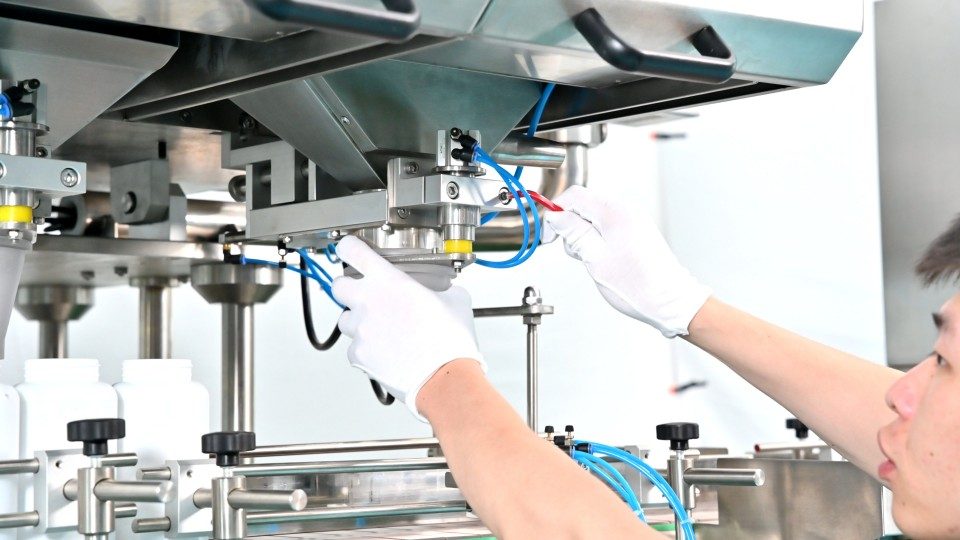
Pharmaceutical Tablet Counting And Filling Machine Changeover
Electronic counting machine changeover affects bottle guides, discharge nozzle, シリンダー, counting platform and more
Cartoning Machine Changeover
箱詰め機 changeover mainly involves adjusting the carton feeding, carton opening, 商品の挿入, folding, 閉店, and inspection sections for the next carton format. Typical setup points include the carton magazine, carton conveying guides, carton-opening mechanism, コンベア幅, pusher mechanism, ear-folding and carton-closing mechanism, and inspection position. These adjustments help maintain stable carton feeding, accurate product insertion, reliable carton closure, and correct inspection during restart.
Ruida Packing applies changeover-focused design to several machine families. 例えば, の ブリスターマシン uses modular molds with slide-out guide rails, allowing tool-free mold replacement in under 14 分. の ロータリー打錠機 allows the dies to be installed by hand without hammering, using flat set screws for faster and more repeatable positioning. On the 自動カプセル充填機, slide-in filling-rod assemblies and quick-positioning upper and lower molds allow a complete standard tooling and filling-system changeover in about 60 分.
Routine changeover is also different from an engineering or system change. A modification to tooling design, recipe logic, software configuration, or another element that can affect product quality may require formal 変更制御 rather than ordinary setup.
Why Does Pharmaceutical Changeover Take So Long?
Changeover becomes slow when necessary controlled work is combined with avoidable searching, waiting, repeated adjustment, and unstable restart.
Cleaning and Product-Contact Part Removal
Cleaning can legitimately consume a large share of changeover time when components must be removed, 掃除された, 検査された, and reassembled. The scope depends on product, 装置, campaign strategy, next use, and the approved cleaning procedure.
Poor Change-Part Organization
Missing or poorly stored change parts turn downtime into search time. The complete part set should be identified and available before the machine reaches that setup step.
Excessive Manual Adjustment
Manual adjustment is slow when machine positions cannot be reproduced reliably. Guides, フィーダー, センサー, and stations that depend heavily on operator judgement often create trial-and-error.
Incorrect or Unavailable Machine Recipes
Recipes save time only when the correct settings match the correct physical configuration. An obsolete recipe, unauthorized change, or wrong product selection can increase troubleshooting.
Waiting for Inspection and Verification
Required verification becomes avoidable waiting when responsibilities and timing were not planned before shutdown. Downtime reduction should improve coordination, not bypass checks.
Repeated Trial-and-Error During Restart
Frequent post-startup tuning indicates that setup is not sufficiently repeatable. ISPE treats startup as a distinct part of changeover and links unstable startup with variation in setup, 製品, or materials.
How Can You Reduce Pharmaceutical Changeover Downtime?
Reduce downtime by removing avoidable work from the stopped-machine period while preserving clearance, クリーニング, 設定, and verification controls.
Separate Internal and External Changeover Activities
Internal activities require stopped equipment; external activities can occur outside that critical downtime window. This distinction is central to Single-Minute Exchange of Die (SMED). Internal activities include removing product-contact parts, tooling changes, mechanical adjustments, and final setup checks. External activities include pre-staging clean change parts, preparing tools and documents, confirming recipes, and organizing required materials before shutdown.
[IMAGE 5 PLACEHOLDER — SMED: Internal vs External Changeover Activities]
Apply SMED Principles
SMED restructures changeover work; it does not promise a universal pharmaceutical changeover time. Map the actual sequence and identify waiting, walking, searching, repeated adjustment, and work that can legitimately move outside machine-stop time.
Pre-Stage Tools, 材料, and Change Parts
Pre-staging keeps preparation work out of production downtime. Check required parts, ツール, and setup information before shutdown while protecting controlled components.
Use Quick-Release and Repeatable Positioning Designs
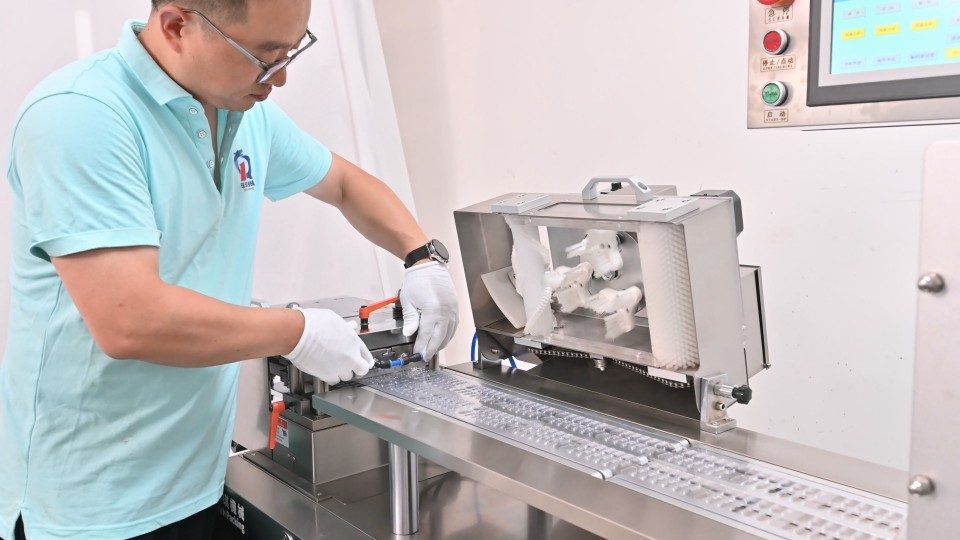
Quick-release features add value when faster removal is paired with repeatable installation. Locating pins, keyed parts, quick clamps, mechanical stops, and modular assemblies can reduce adjustment.
Standardize HMI Recipes and Machine Settings
Controlled recipes help reproduce known parameter sets. Recipe identification, authorized access, configuration control, and traceability remain important for GMP-relevant data.
Use Position Scales, Reference Marks, and Setup Records
Repeatable reference points reduce post-changeover tuning. Scales, mechanical stops, servo positions, and documented setup values can return guides, センサー, and feeders close to established positions.
Run Parallel Tasks Where Possible
Independent activities can run in parallel when safety, GMP controls, and task dependencies allow it. The objective is to remove unnecessary serial waiting.
Standardize Restart Verification
A defined restart check gives changeover a clear endpoint and reduces uncontrolled trial-and-error. Each equipment family should define what must be checked before routine production resumes.
What Are the Most Common Pharmaceutical Changeover Mistakes?
The most common mistakes occur when physical parts, electronic settings, 書類, and verification do not describe the same production configuration.
Typical examples include wrong or incomplete format parts, sensors left in the previous position, wrong or uncontrolled recipes, unresolved line-clearance discrepancies, unrecorded setup references, missed coding or inspection changes, and release before restart checks.
Repeated correction of the same sensor, ガイド, レシピ, or tooling position is a candidate for standardization. If a discrepancy can affect product quality or departs from an approved procedure, it should enter the site’s deviation or quality-system process rather than being hidden by repeated machine adjustment.
How Should Changeover Performance Be Measured?
Changeover performance should use consistently defined measures covering time, startup stability, material loss, and production recovery.
切り替え時間
Changeover time is useful only when its measurement boundary remains consistent. Use the same start and end points across products, 行, shifts, and improvement projects.
First Good Product After Restart
First-good-product performance shows whether setup produces acceptable output without prolonged tuning. Faster tooling replacement is not an improvement if restart still needs extended adjustment.
Startup Scrap and Rework
Startup scrap captures the material cost of unstable restart. It reveals losses that a downtime-only metric can miss.
Changeover-Related Downtime
Downtime becomes more actionable when divided into causes. Useful categories include cleaning, ラインクリアランス, mechanical setup, waiting, 検証, and restart adjustment.
OEE and Production Availability
全体的な機器の有効性 (OEE) and availability provide context but should not replace direct changeover measures. 国際調和評議会 (私) Q10 supports process-performance monitoring and continual improvement but sets no universal changeover target.
よくある質問
What is a pharmaceutical production changeover?
It is the controlled transition from one production condition to another, including the required clearance, クリーニング, 設定, startup, and verification activities.
Does every pharmaceutical changeover require the same cleaning procedure?
いいえ. Cleaning scope depends on product, 装置, campaign strategy, previous and next use, and the approved cleaning procedure.
What is the difference between changeover and line clearance?
Changeover is the complete transition; line clearance is one control within it. Tooling changes, 設定, recipes, and restart verification are separate activities.
What is the difference between cleaning and line clearance?
Cleaning removes residues and contaminants; line clearance removes previous or incorrect materials and information. One does not automatically replace the other.
How long should a pharmaceutical changeover take?
There is no universal time. Duration depends on equipment, product differences, cleaning scope, format complexity, verification requirements, and the measurement boundary.
How can pharmaceutical changeover time be reduced?
Remove avoidable work rather than required controls. Pre-stage parts, separate internal and external work, standardize settings, coordinate tasks, and reduce restart tuning.
What is SMED in pharmaceutical manufacturing?
SMED is a method for reducing setup time by separating internal and external activities. GMP-related clearance, クリーニング, ドキュメント, and verification still remain.
What are change parts in pharmaceutical machinery?
Change parts are components replaced or repositioned for another product or package format, such as punches, 死ぬ, capsule-size parts, ブリスター型, ガイド, もっと.
How is pharmaceutical changeover performance measured?
Useful measures include changeover time, first good product, startup scrap, changeover-related downtime, and availability. Consistent definitions are essential.
結論は
A faster pharmaceutical production changeover must still preserve controlled line clearance, クリーニング, equipment setup, parameter verification, and restart quality.
The strongest improvements come from removing avoidable searching, waiting, repeated adjustment, and startup trial-and-error while keeping required controls intact. 評価する 製薬機械 not only by rated speed, but by what must be cleaned, changed, adjusted, reproduced, and verified before routine production resumes.
参考文献
欧州委員会. EudraLex ボリューム 4, Part I, 章 5: 生産, Section 5.45.
私たち. 食品医薬品局. Guide to Inspections: 洗浄プロセスの検証 (7/93).
欧州委員会. EudraLex ボリューム 4, 別館 11: コンピュータ化されたシステム, Sections 9–12.
Lean Enterprise Institute. Single-Minute Exchange of Die (SMED).
世界保健機関. WHO の医薬品の適正製造基準: Main Principles. TRS 986, 別館 2, 2014.
電子連邦規則集. 21 CFR §211.130: Packaging and Labeling Operations.